 View Mazlum Boru on TEKEN44
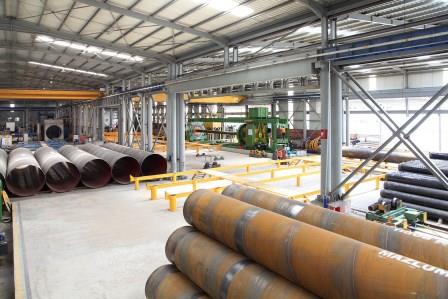
Internal and External Welding Immediately after the pipe forming process, inside welding is carried out around 30 mm behind the edge contact point by submerged arc welding process. Followed by half helical turn which depending on machine design external welding is carried out depending on pipe diameter and wall thickness; in addition to the individual and relative. All the welding parameters (Current, voltage, speed and etc.) and welding consumables are specified in Welding Procedure Specifications Ultrasonic Inspection The produced pipes are control and record by Automatic On-Line Ultrasonic Control and computer systems. The faultless pipe production is realized by applying advanced ultrasonic evaluation system and program. The produced pipes are performing body and HAZ lamination and weld seam testing. The length cutting shall be carried out by plasma cutting method according to customer specification.
API 5L
Specification for Line Pipe...
ISO 3183
Petroleum and natural gas industries — Steel pipe for pipeline transportation systems
EN 10219-1
Cold formed welded structural hollow sections of non-alloy and fine grain steels - Part 1: Technical delivery conditions
EN 10217-1
Welded steel tubes for pressure purposes - Technical delivery conditions - Part 1: Non-alloy steel tubes with specified room temperature properties
EN 10224
Non-alloy steel tubes and fittings for the conveyance of aqueous liquids including water for human consumption - Technical delivery conditions
TEKEN44 Similar Products


Google Lens Search · visually similar products
The TEKEN44 product image was analyzed with Google Lens via the TEKEN44 MCP server to find 20 visually similar products from across the web.